Boksburg stock for mixed metal cutting
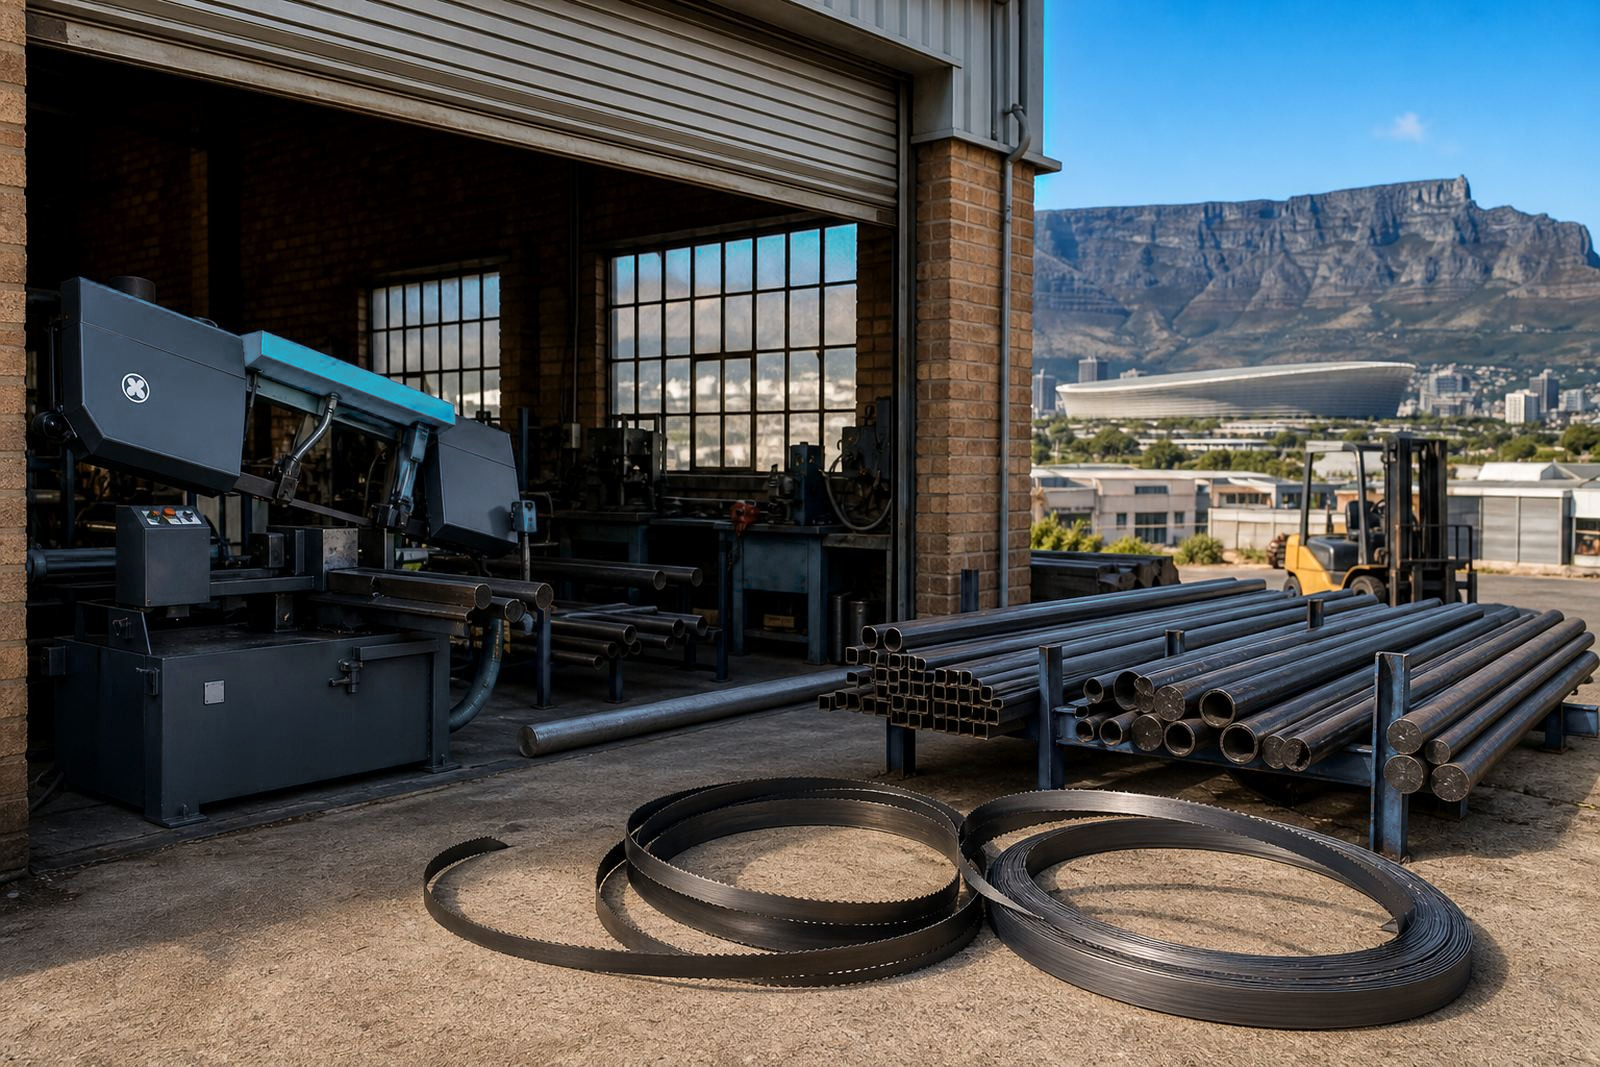
The Boksburg Supply area covers shops and workshops that cut a wide mix of material, often in short runs and with different machines on the same floor. We cover bandsaw blades and hacksaw blades for mild steel, structural sections, solid bar, thin wall tube and general repair work, with lengths welded to suit the machine rather than forcing a bad fit.
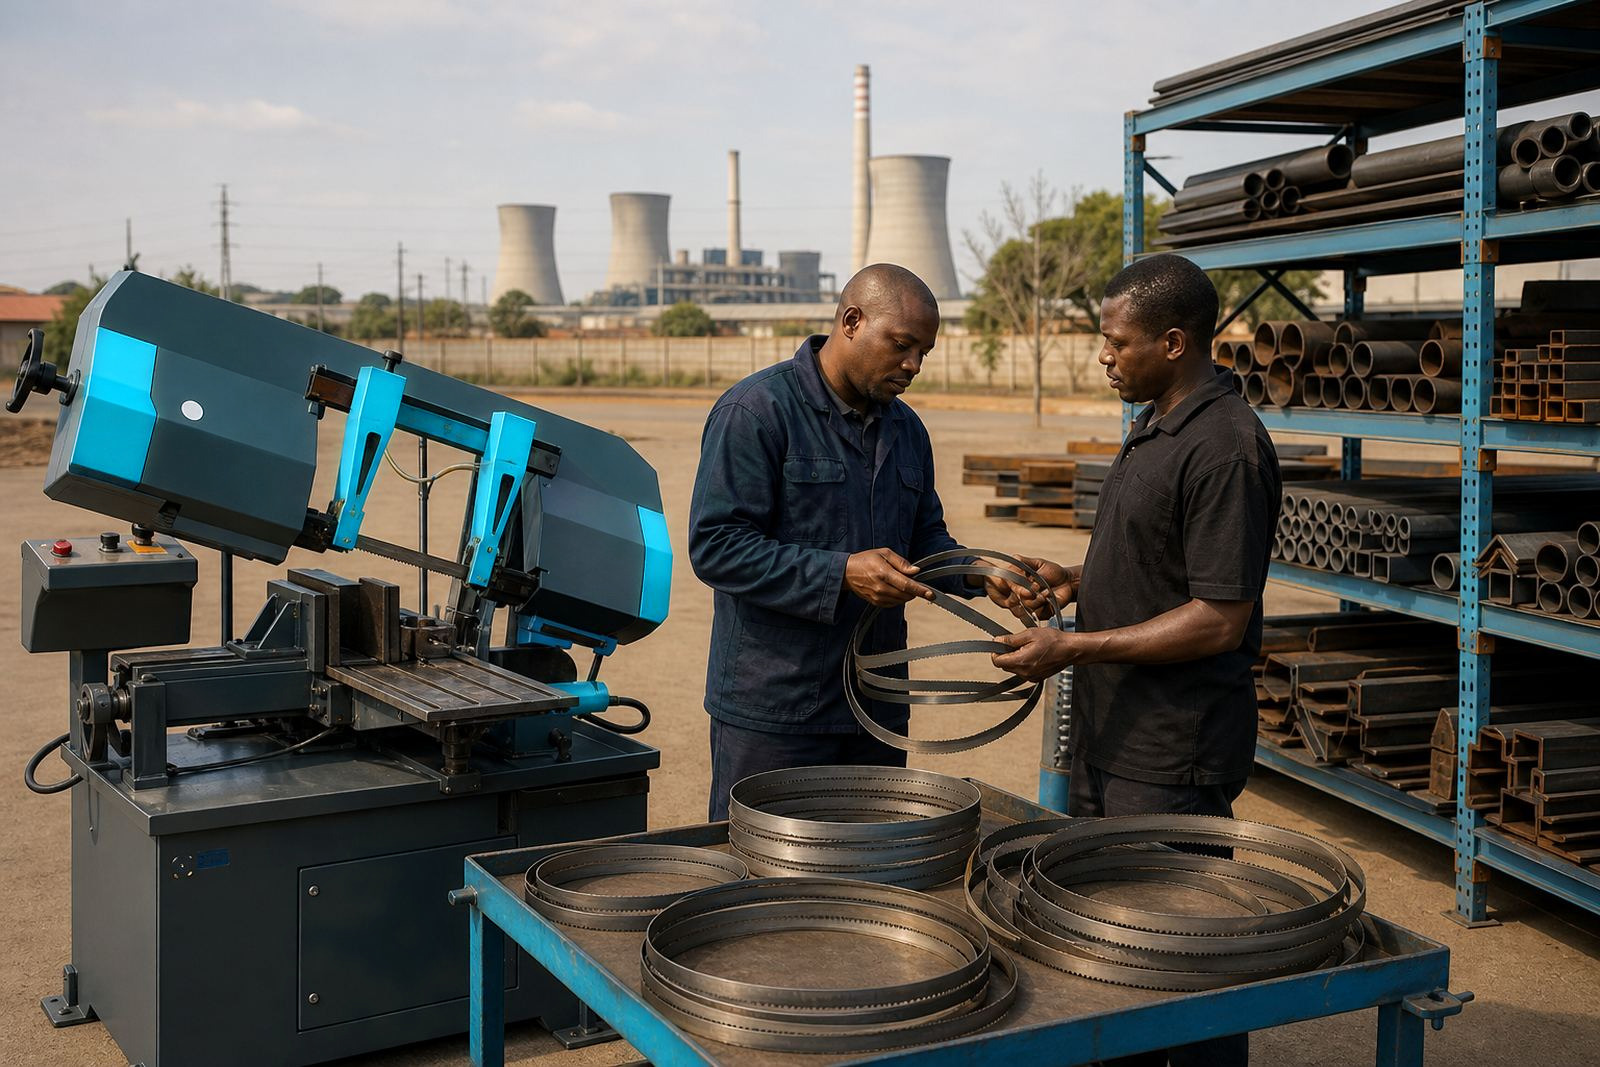
Stock choices usually come down to tooth pitch, blade width, thickness and the way the blade is set for the cut. A finer pitch helps with thinner sections and small-diameter tube, while a coarser pitch suits heavier sections and solid material. Variable pitch options can calm chatter on mixed jobs, and the right set helps the blade clear chips instead of rubbing and heating up.
- Bi-metal blades for tougher workshop use
- Carbon steel blades for lighter manual and light duty work
- Starter kits for new saws or fresh blade planning
- Welded loops cut to the machine length required
How local workshops usually use these blades
Boksburg has plenty of fabrication, maintenance and repair work, plus subcontract cutting for nearby factories, steel merchants and jobbing shops. Many teams need a blade that can handle interruptions, off-cuts and changing material grades without constant swapping. For that work, choose the tooth pitch and blade width first.
For a manual saw, feed pressure and speed need to stay steady enough for the teeth to bite cleanly. For powered bandsaws, the right running speed and feed prevent tooth stripping and keep the cut square. We also check coolant, especially on longer cuts or when the material gets warm through repeated work. In humid conditions or where machines sit near open yard space, rust film and dirty coolant can shorten blade life if nobody watches the basics.
Our workshop support covers blade failure review too. If a blade breaks early, runs off line or leaves a rough finish, we look at the tooth pitch, the machine fit, the guide set-up and the actual cut material before recommending the next blade spec.
- General fabrication and maintenance shops
- Steel cutting counters and jobbing workshops
- Machine shops working with round, flat and section stock
- Manual saw users needing steadier blade control
Weld-to-length service for the Boksburg side
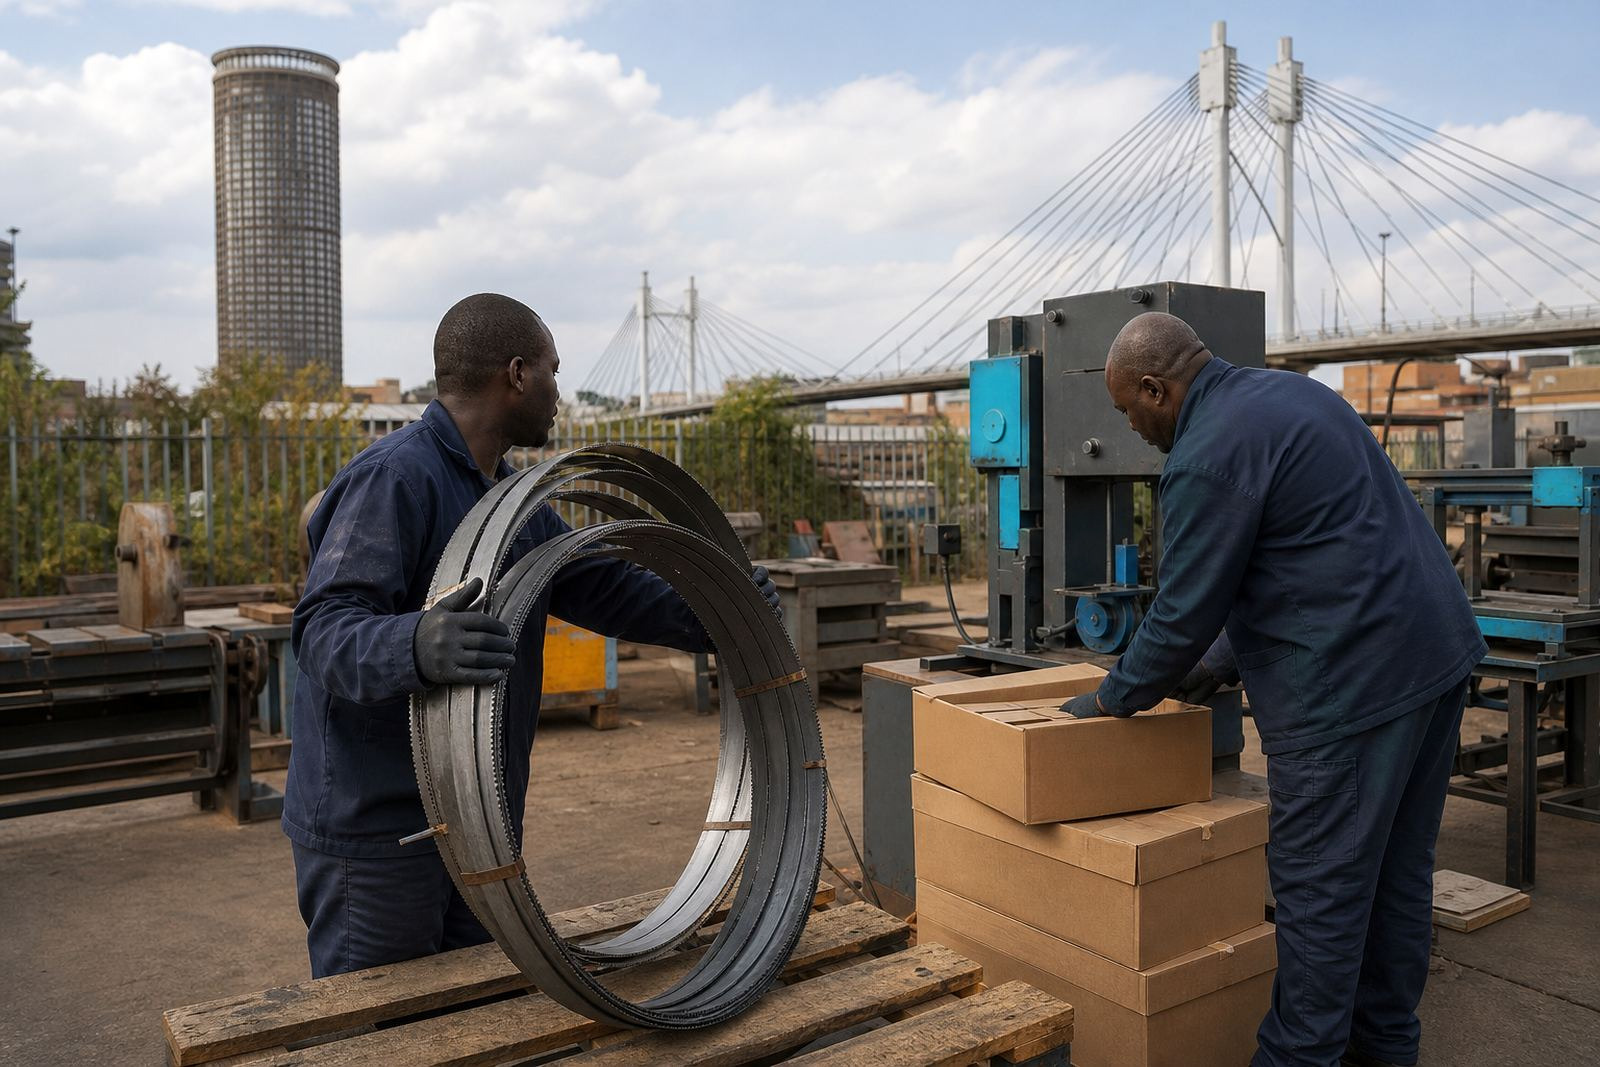
Blade welding is part of the service because many machines need a closed loop made to exact length. If the loop is too tight the blade can track badly, if it is too loose it loses control. We weld to the machine length, then check the loop and finish so the blade sits correctly on the saw wheels and guides.
Length verification goes together with machine fit check. A blade can be the right pitch and still perform poorly if the length is off by a small amount or the guides are worn. On-site machines in Boksburg often work hard and the cut results are only as good as the fit, alignment and feed the operator gives it.
- Weld-to-length loops for common workshop saw sizes
- Length verification before supply where the machine details are supplied
- Machine fit checks for guide and wheel compatibility
- Blade failure review when a cut pattern keeps repeating
Starter kits and blade planning for smaller shops
Smaller Boksburg workshops often want a sensible starting point rather than a long list of options. Starter kit planning helps match the first blade set to the machine, the most common material and the way the team actually works. That usually means one reliable bi-metal choice, one finer pitch for thin wall work and a coarser option for heavier sections.
Stock standardisation helps too. When a workshop keeps one or two clear blade patterns across similar saws, it becomes easier to track wear, set up ordering and train operators on the same cut approach. Busy bays need this when different staff use the saw during the week. It also cuts down on wrong blades being fitted just because they were on hand.
We also cover run-in guidance. New blades need a controlled first period so the teeth bed in properly before they are used on hard material. If the run-in is skipped, the edge can chip early and the cut line starts to wander.
- Starter kits for new operators or new machines
- One blade set across similar saws
- Run-in guidance for fresh blades
- Manual saw support where the cut depends on operator control
What reaches Boksburg and when
Boksburg sits close enough to Johannesburg and Germiston for quick movement of stock, yet each workshop still needs the right blade in the right length. Our area cover includes Boksburg Supply, with support also flowing through to nearby east Rand workshops that cut steel every day. We supply the correct blade for the job, the machine and the material thickness.
We stock and cover common bandsaw and hacksaw requirements for metalwork, including bi-metal M42 type blades, carbon steel blades, variable pitch options, different widths and thicknesses, and the practical details that keep the cut stable. Tooth pitch selection remains central, because a blade that is too fine loads up on heavier stock, while one that is too coarse leaves a rough cut on lighter sections. Feed speed advice and coolant checks complete the picture, especially on repetitive cutting where the machine can drift from good habits.
Send the machine length, material type, section size and whether the blade is for a bandsaw or a hacksaw setup.
- Bandsaw blades for mixed workshop cutting
- Hacksaw blades for manual and bench work
- Blade width and thickness matched to the machine
- Coolant and feed checks for cleaner cutting
Typical Boksburg jobs we cover
Many Boksburg teams cut steel that changes from one order to the next, so blade selection has to stay practical. A thin-wall tube job does not call for the same tooth pitch as a short run of solid round bar, and a blade that works on one saw may not suit the next machine at all. Enquiry details help when a shop uses more than one saw or changes operators often.
We support fabricators, maintenance teams, repair shops and small production bays that need clear guidance without overcomplicating the job. We match blade type, pitch, width and set to the work, then keep the machine fit checked so the blade does what it should. For Boksburg, that usually means practical help, sensible stock and welded lengths ready for the saws already in service.
If the blade leaves burrs, heats up too fast or throws chips badly, the fix is often in the pitch, feed or coolant rather than the operator forcing the cut. We look at those details first and keep the advice tied to the material on the bench.